Distilleries Filtration Engineering
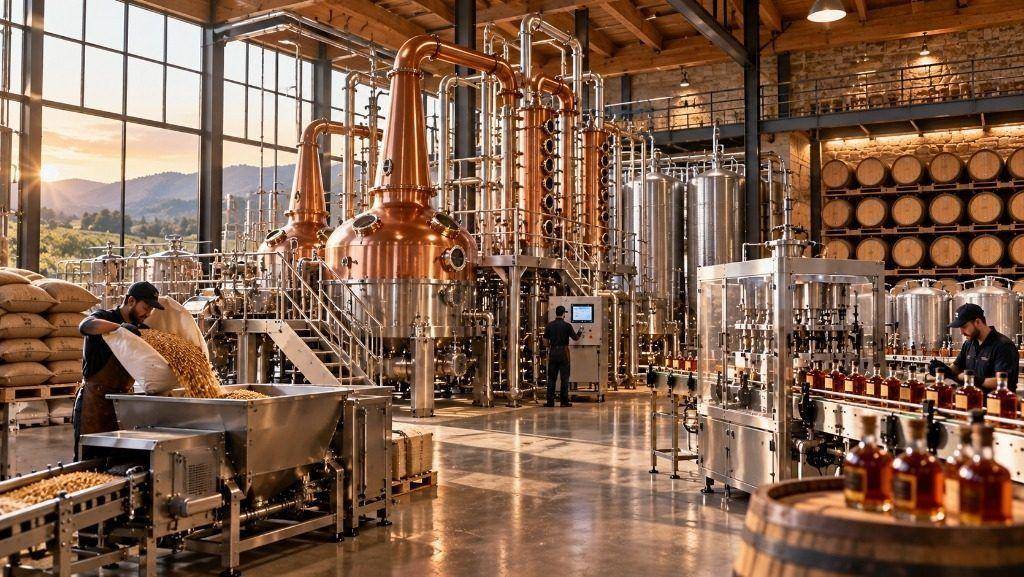
Trinity Filtration delivers comprehensive liquid separation and purification technologies for commercial distilleries (whiskey, rum, vodka, gin) and packaged bottled water plants. In spirits production, our sub-zero chill proofing cartridges and activated carbon blocks eliminate lipid haze and barrel char while preserving rich aromatics. For bottled water and mineral water facilities, our high-flow sediment filters, carbon blocks, and 0.2 µm absolute STERIPRO PES sterile membrane cartridges ensure complete bioburden removal, cryptosporidium barrier, and optical sparkle.
Critical Separation Challenges
Key operational bottlenecks, bioburden risks, and compliance challenges in Commercial Distilleries & Bottled Water Plants.
Chill Haze in Diluted Whiskey & Rum
Fatty acid ethyl esters (ethyl laurate, palmitate, oleate) become insoluble when spirits are chilled or proof-diluted, causing unacceptable cloudiness.
Oak Barrel Char & Wood Splinters
Aging in charred white oak casks imparts amber color and rich tannins but releases heavy carbon grit and wood particles that clog downstream lines.
Cryptosporidium & Bioburden in Bottled Water
Packaged drinking water plants require absolute microbial barrier against waterborne cysts, bacteria, and Pseudomonas without adding chemical disinfectants.
Off-Flavor & Harsh Congeners in Vodka & Water
Trace organic congeners in neutral spirits and residual chlorine/trihalomethanes in municipal feed water require high-adsorption coconut shell carbon block filtration.
Process Flow & Engineered Solutions
Engineered multi-stage filtration loops and precision separation media designed for maximum process yield in Distilleries.
Raw Water & Cask Dumping Pre-Filter
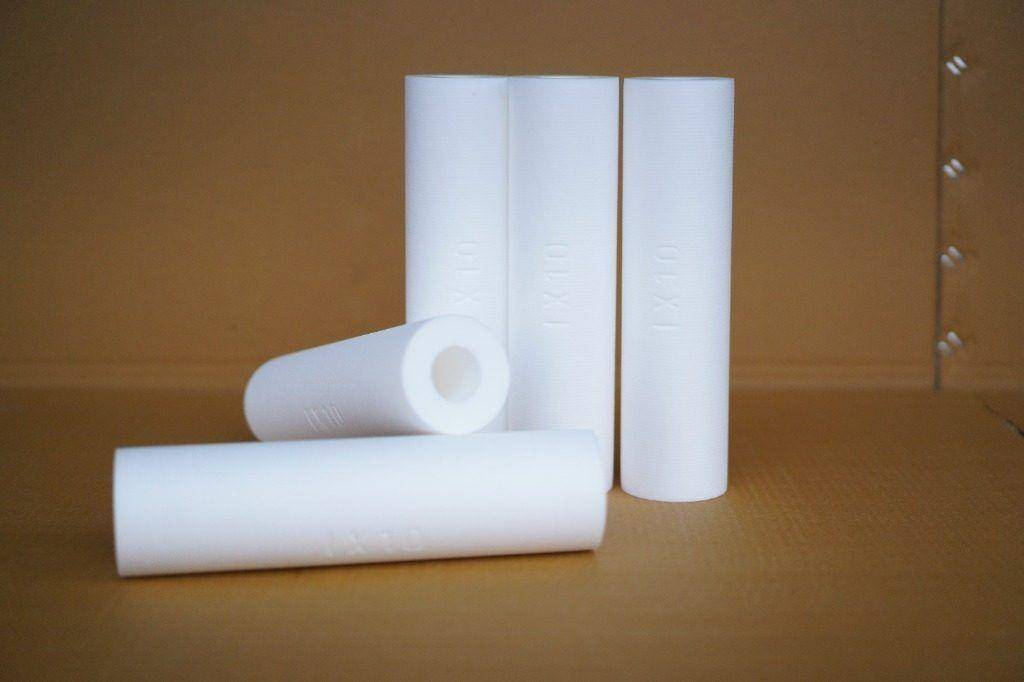
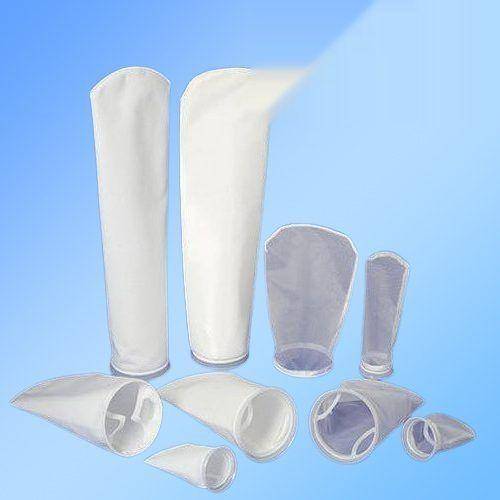
High Flow 6" cartridges and Flow Pure needle felt bags capture heavy intake sediment, silt, and barrel char particulates (5–25 µm).
Sub-Zero Chill Proofing (-4°C)
Pure Guard bi-component depth cartridges selectively trap precipitated fatty acid esters and lipids while preserving authentic cask aromatics.
Activated Carbon Flavor & Odor Polishing
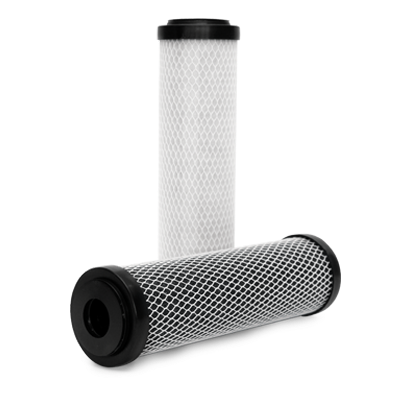
Extruded coconut shell carbon block cartridges adsorb unwanted fusel oils, color haze in vodka, and chlorine/chloramines in bottling water with zero carbon bleed.
0.2 µm Sterile Bottling Membrane Guard
STERIPRO PE (PES) 0.2 µm absolute sterile membrane filters provide 100% microbiological retention, cyst barrier, and crystal optical sparkle before bottle filling.
Filtration Products for Distilleries & Bottled Water
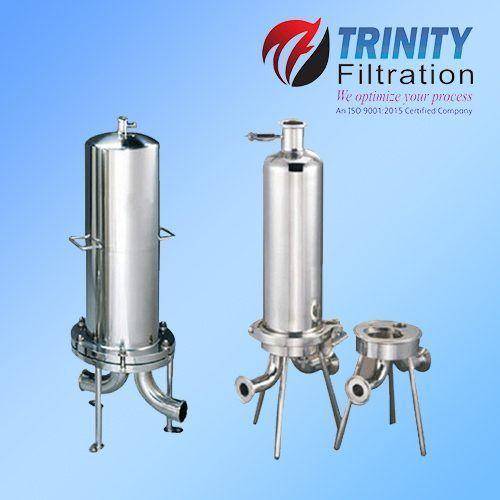
Proven filter elements, sanitary vessels, and purification skids selected for this sector.